PVC Antistatic Flooring Factory: Inside the Production of Safe, Static-Free Industrial Floors
2026-09-16
静电可能是工业环境中最隐蔽的杀手——一次微小的火花就足以毁掉精密设备甚至引发爆炸。走进 Lipin Floor 的 PVC 防静电地板工厂,你会发现这些看似普通的地板如何通过精密的导电配方与层层质检,成为真正“零静电”的安全屏障。从原料混合到压延成型,每一步都藏着不为人知的工艺秘密。准备好揭开无静电工业地板的制造之谜了吗?
Raw Materials That Set the Static-Free Stage
Anti-static protection starts long before a product is assembled—it begins with the raw materials themselves. Conductive polymers, carbon-loaded polyethylene, and metalized fabrics are chosen not only for their durability but for their natural ability to shed electrostatic charge. Each material brings a distinct balance: some dissipate charge gradually, while others ground it instantly, giving engineers a toolkit that adapts to sensitive components and unpredictable handling environments.
The real craft lies in blending these substances without compromising mechanical strength or thermal stability. Additives like graphite powder, conductive carbon black, or ionic surfactants are mixed into base resins at precise ratios, turning an ordinary plastic into a controlled pathway for electrons. In textile applications, copper or silver threads are woven into polyester strands, creating garments that stay static-free even after repeated laundering—no surface treatment that wears off, but a structural property built into every fiber.
Selecting the right base material often depends on the target surface resistivity, which can range from dissipative to fully conductive. For instance, a polyurethane foam infused with carbon nanotubes may cushion a circuit board while bleeding away charge, whereas a rigid polypropylene tote with a permanently anti-static additive protects components during transit. These choices aren't standardized; they demand lab testing under humidity extremes and abrasion cycles, ensuring the material won't suddenly become an insulator when it matters most.
Calendering Lines Where Consistency Meets Conductivity
In the world of electrode manufacturing, the calendering line is where raw coated foil transforms into a precisely engineered layer. Here, two critical demands converge: uniform thickness for consistent electrochemical performance, and compressed porosity that keeps ionic pathways open for conductivity. The rollers apply controlled pressure, but the real art lies in maintaining that balance across every millimeter of the web, from start to finish.
Operators watch tension, gap, and temperature closely because small deviations can create weak spots or density variations. A well-tuned calendering line doesn't just squeeze material—it aligns the active particles, reduces internal resistance, and helps the final cell deliver stable capacity over hundreds of cycles. That's why consistency isn't a byproduct; it's built into the machine's rhythm.
Modern lines push this further with closed-loop thickness gauging and roll bending compensation, so the same conductivity target is hit at the edges as in the center. In practice, that means fewer rejected rolls, tighter scrap rates, and electrodes that behave predictably when stacked or wound. When consistency and conductivity meet on a calendering line, the result is more than a compressed strip—it's the foundation for reliable energy storage.
Building the Conductive Core Layer by Layer
Creating a truly reliable conductive core isn't about dumping everything in at once. It starts with a thin, uniform base that grips the substrate—often a sputtered or chemically deposited seed layer no thicker than a few hundred nanometers. That initial film sets the texture and adhesion profile for everything that follows, and if it's patchy, no amount of later plating will fix the weak points. Builders who rush this step usually end up fighting delamination or uneven current distribution down the line.
Once the seed is in place, the real structural work begins. Alternating electroplating and brief etching cycles can fill trenches and vias from the bottom up, rather than letting sidewalls close off too early. Each pass adds a controlled amount of metal—copper, silver, or a composite—while the etch step trims high spots and exposes fresh nucleation sites. The rhythm matters: shorter pulses with tight current density control produce denser grain structures, which lowers resistivity and improves electromigration resistance. It's the difference between a core that survives thermal cycling and one that develops micro-voids after a few hundred hours.
Finally, a capping layer locks the stack together. This might be a thin nickel or cobalt alloy that prevents oxidation of the main conductor and provides a stable surface for wire bonding or soldering. By building up the core in distinct, purpose-driven layers—seed for adhesion, bulk for conductivity, cap for protection—you avoid the brittleness and internal stress that single-step deposition almost always introduces. It's slower, yes, but each layer earns its place.
Real-World Testing for Static Dissipation Performance
Static dissipation isn’t something you can fully verify on a spec sheet alone. In real facilities, the way a floor actually performs depends on a mix of footwear, humidity, cleaning routines, and daily wear patterns. That’s why field testing matters — it captures how the surface behaves under conditions that a controlled lab simply can’t replicate.
One common approach is to take resistance measurements at multiple points across a working floor, not just near the grounding points. You’ll often see values drift higher in areas with heavy cart traffic or where polish has built up over time. Comparing readings before and after a shift gives a more honest picture than a single spot check done right after installation.
Walk tests with different shoe soles also reveal a lot. Some combinations of flooring and footwear generate enough static to cause nuisance shocks or disrupt sensitive electronics, even when the material passes bench tests. Watching how people actually move through the space — and measuring voltage in those moments — is what separates a floor that meets a standard from one that works in practice.
Custom Surface Finishes for Tough Industrial Settings
Industrial environments rarely offer a one-size-fits-all answer when it comes to surface protection. A chemical processing plant dealing with constant acid splashes demands a completely different finish than a food packaging facility scrubbed hourly with hot water and caustic cleaners. That's why we build every coating system from the substrate up, matching resin chemistry, cure schedule, and film thickness to the specific abuses your floors, walls, or equipment will face. Rather than forcing a generic epoxy onto every surface, we start by mapping wear patterns, thermal cycling, and exposure levels, then adjust aggregate blends and topcoats accordingly.
The real difference shows up months later, when a standard floor would be showing micro-cracks and delamination. Our custom finishes are formulated for the long haul: high-solids polyurethanes that flex instead of fracture under forklift traffic, trowel-applied cementitious urethanes that shrug off thermal shock from steam washdowns, and anti-static systems that prevent spark hazards in solvent storage areas. We also pay attention to what happens at the edges—cove bases, drains, and expansion joints—because that's where most industrial failures begin.
What sets a tailored approach apart is not just the chemistry but the timing. We coordinate curing windows around your production downtime, use moisture-tolerant primers when slabs can't fully dry, and offer accelerated topcoats that let you resume operations within hours instead of days. No two job sites are alike, and your finish shouldn't be either. If your current surface is failing in predictable ways, it's usually a sign that someone sold you an off-the-shelf solution for a custom problem.
Leaving the Factory with Every Roll Ready to Install
Every roll gets a final pass through a tension-check station before it earns a pallet spot. The winding tension is matched to the substrate's stretch profile, so a 50-meter run unrolls with the same flatness at the last meter as at the first. If a splice or a thin spot shows up under the inspection light, that section is cut out and the roll is re-taped with a clean, labeled start edge.
The core itself carries printed hash marks every 30 centimeters, not as decoration but as a quick reference for installers who need to align seams or match a pattern repeat. Each roll is sealed in a low-tack film that peels away without leaving residue, and the tail is secured with a color-coded band that tells you the unwind direction before you even lift the roll.
What arrives on site is not a raw material that still needs sorting, trimming, or tension guesswork. It is a finished unit: consistent diameter, factory-set tension, marked edges, and no hidden splices. Open the box, mount the roll, and the first pull is as ready as the last.
FAQ
A dedicated line uses conductive carbon-loaded PVC wear layers and a buried copper or aluminum grounding grid. Workers constantly check surface resistance with megohmmeters, and rooms are kept at controlled humidity because static dissipation changes with moisture. You won't see standard vinyl being handled with the same grounding straps and ESD footwear requirements.
Conductive additives like carbon black, graphite, or carbon fiber are compounded into the PVC mix. This creates a network of pathways that let charges bleed off to a grounded copper foil layer or conductive adhesive. The target is usually between 1x10^6 and 1x10^9 ohms surface resistance, which is low enough to avoid static buildup but high enough to protect workers from electrical shock.
Semiconductor fabs and electronics assembly plants need them so a small discharge doesn't fry microchips. Munitions and chemical facilities use them to prevent sparks that could trigger explosions. Hospital operating rooms and data centers also install them to protect sensitive equipment and anesthetic gases. In each case, even a 100-volt static zap can be too much.
You start by blending PVC resin with plasticizers, stabilizers, and conductive filler. That mix is heated and calendared into sheets, then laminated with a conductive backing and sometimes a glass-fiber core for dimensional stability. After hot pressing, the sheets are cooled, cut into tiles or planks, and left to cure for a day or two before resistance testing. It's less about a single secret step and more about consistent control of filler dispersion and temperature.
Each production lot sits in a conditioning room at 23 degrees Celsius and 50 percent relative humidity for at least 24 hours. Technicians then take multiple readings with a surface resistance meter using five-pound electrodes. They also run walking tests to see how much voltage a person generates. If any tile falls outside the accepted range, the whole batch is rejected or reworked.
Applying ordinary floor wax or polish can coat the surface and block the conductive network. Using a non-conductive adhesive or failing to connect the copper grounding strips to earth is another common error. Cleaning with harsh solvents or abrasive pads can wear away the conductive top layer. Also, replacing furniture with non-ESD casters can reintroduce static.
Yes, but the pigments and inks must be specifically formulated to be static-dissipative. Many factories use conductive color concentrates and heat-welded conductive vinyl strips for markings. Custom logos are usually screen-printed with carbon-loaded ink and then sealed with a thin conductive coating. The key is testing after customization to confirm the surface resistance still falls in the safe range.
Tiles usually run from 2mm to 5mm thick, with a wear layer between 0.3mm and 1.0mm depending on foot and cart traffic. Heavy-duty areas like electronics warehouses often choose 3mm or thicker with a 0.7mm wear layer. The conductive properties are built through the entire thickness, not just the topcoat, so deeper scratches don't immediately destroy the static control.
Conclusion
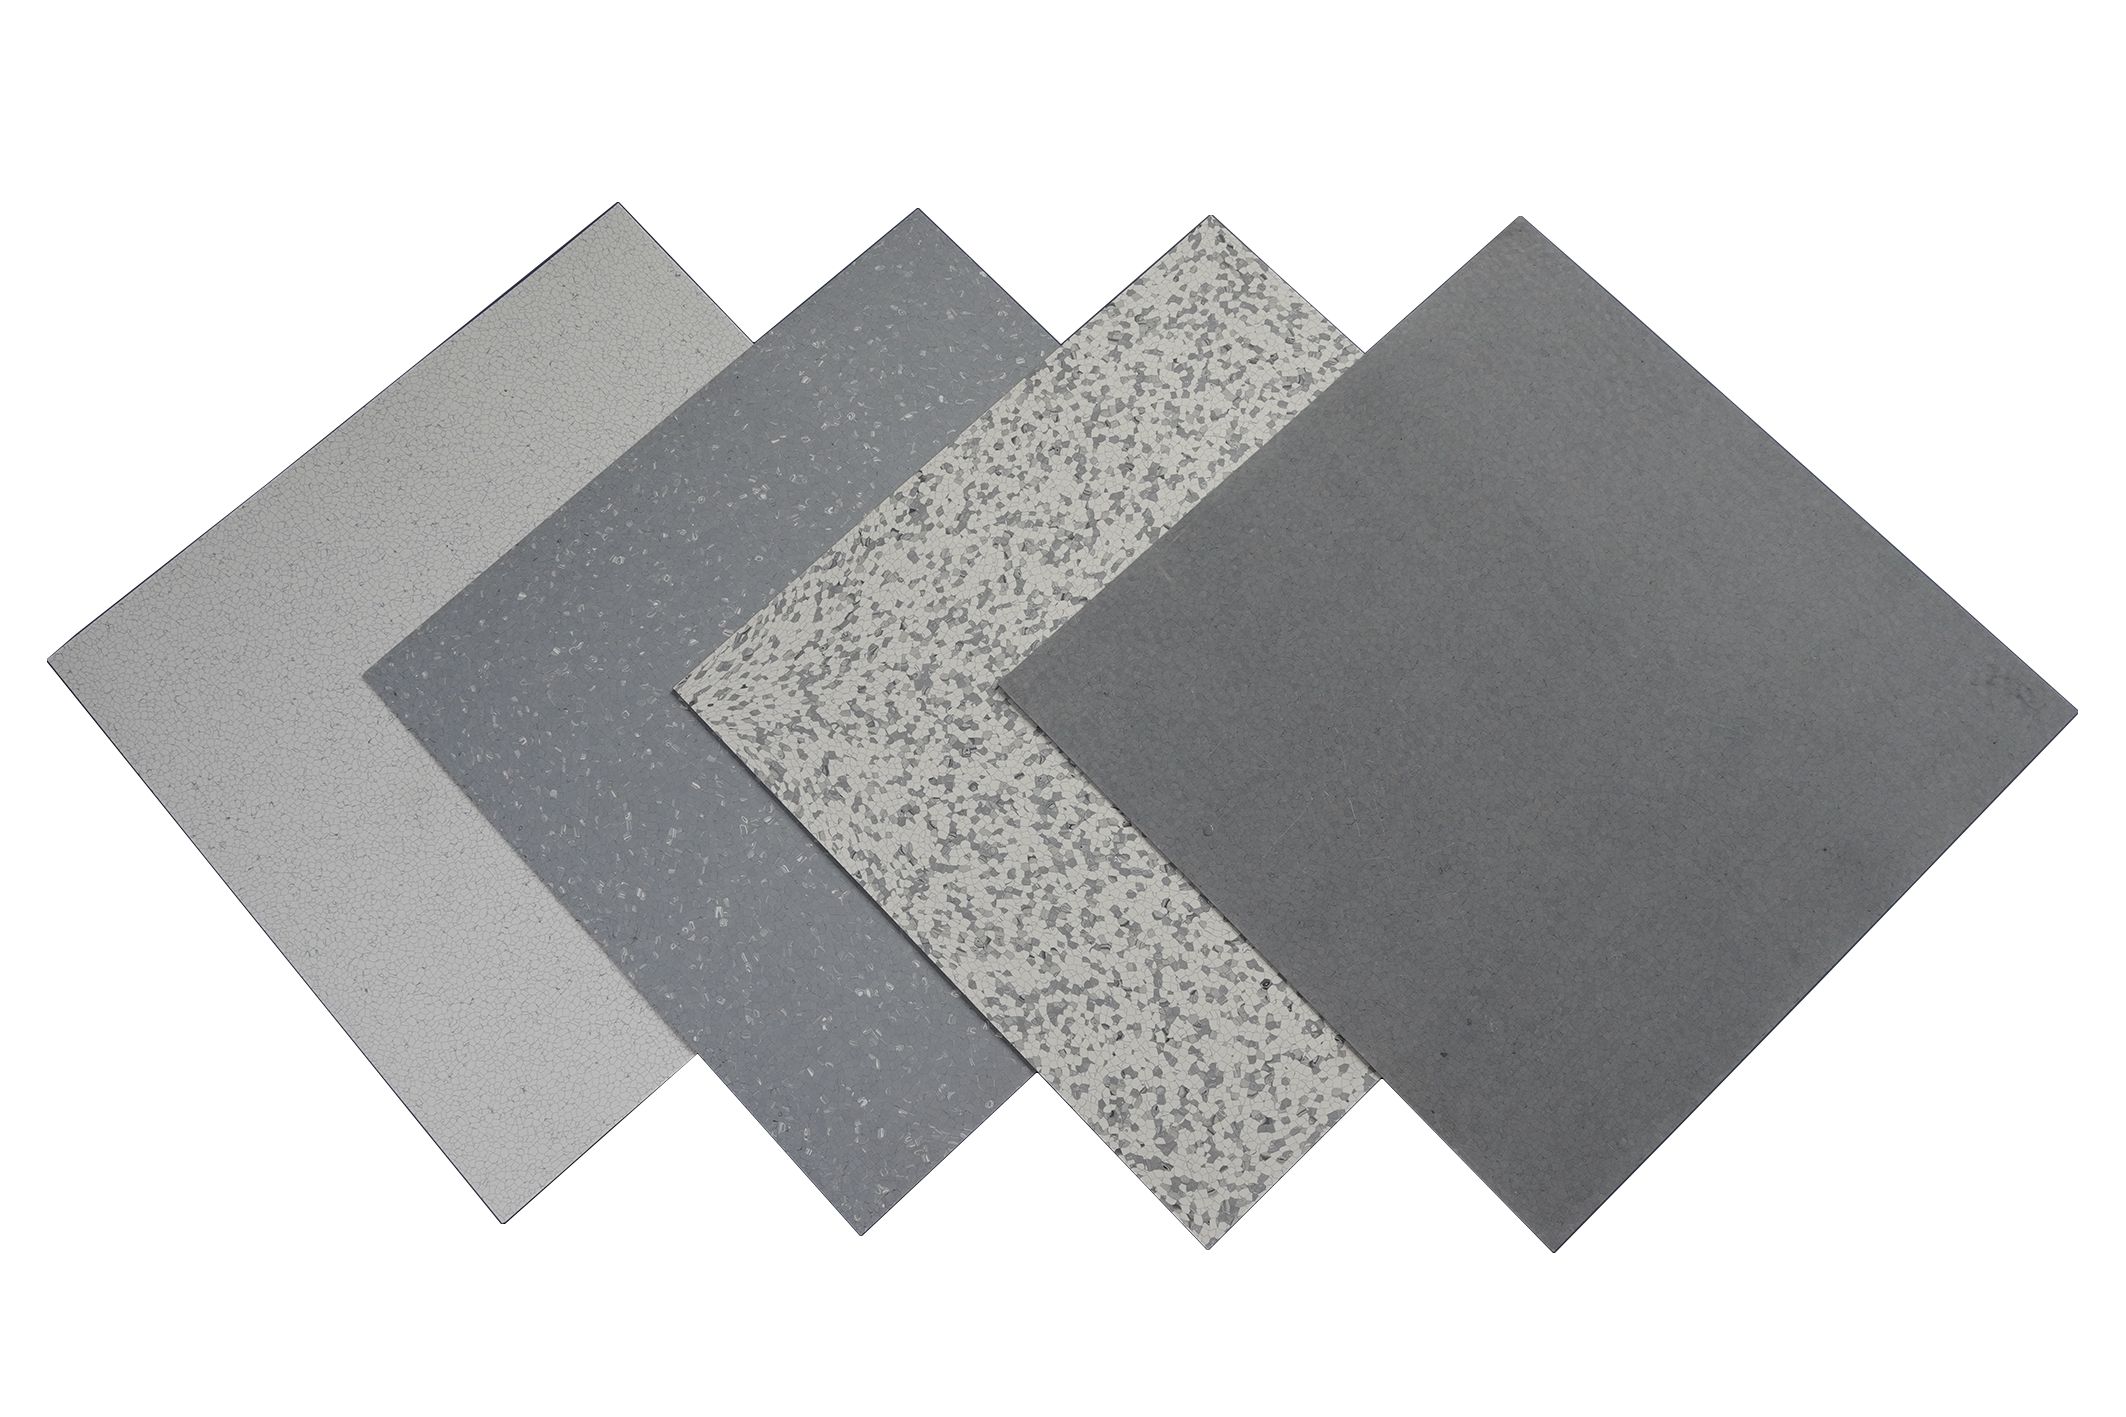
Inside a PVC antistatic flooring factory, the journey begins with a carefully selected mix of raw materials—PVC resins, plasticizers, conductive carbon black, and specialized additives—each chosen to establish a permanent static-dissipative pathway. These ingredients are fed into high-precision calendering lines, where heat and pressure fuse them into uniform sheets while embedding consistent conductivity across every meter. The core is built layer by layer: a conductive underlayer locks in the electrical network, a middle layer adds mechanical strength, and a wear-resistant top layer protects against abrasion. This multilayer construction ensures that the floor does not merely rely on a surface coating but distributes static charges throughout its entire thickness.
Once formed, the rolls undergo rigorous real-world testing for static dissipation, measuring surface and volume resistance under varying humidity and temperature conditions. Custom surface finishes—from embossed textures for slip resistance to high-gloss coatings for cleanroom aesthetics—are then applied to meet the demands of tough industrial settings, including electronics assembly, chemical storage, and operating theaters. Finally, every roll is inspected, trimmed, and packaged with clear installation guidance, leaving the factory ready to be laid directly over existing substrates. The result is a safe, static-free floor that combines reliable performance with practical durability for demanding environments.
Contact Us
Contact Person: yuki
Email: [email protected]
Tel/WhatsApp: +86 18664390732
Website: https://www.lipinfloor.com/